Why Choose Appliance Injection Parts for Global Sourcing?
Global sourcing for Appliance Injection Parts is not simply a search for the lowest unit price. It is a decision about repeatable quality, tooling life, delivery resilience, and the cost of every rejected component. Grand View Research valued the global home-appliances market at about USD 763.45 billion in 2023, underscoring the scale of demand for dependable components. Market size alone, however, does not guarantee a capable supplier.
A well-managed sourcing process starts with practical evidence. Ask for material certificates, dimensional inspection records, tool-maintenance plans, and samples molded under production conditions. Check details that matter on the factory floor: a refrigerator hinge that fits without rework, a washer housing with consistent wall thickness, or a control-panel bezel with clean edges. The International Organization for Standardization’s ISO 20457 provides a framework for tolerances and acceptance conditions for molded plastic parts. It helps buyers define expectations before production begins.
Price is only one measure. Small process differences can create costly surprises.
A sourcing article should not assign an invented quotation to an expert. John Beaumont’s technical work on injection molding is a useful reference for process understanding, but a verbatim quote requires checking against the original publication. That caution matters: credible sourcing depends on verifiable evidence, not polished claims. For buyers comparing Appliance Injection Parts suppliers, the strongest choice is the one that can show how its materials, tooling, inspection, and communication support consistent parts across repeat orders.
Define Appliance Injection Parts in the Context of 400.3 Million Tonnes of Plastics Produced in 2022
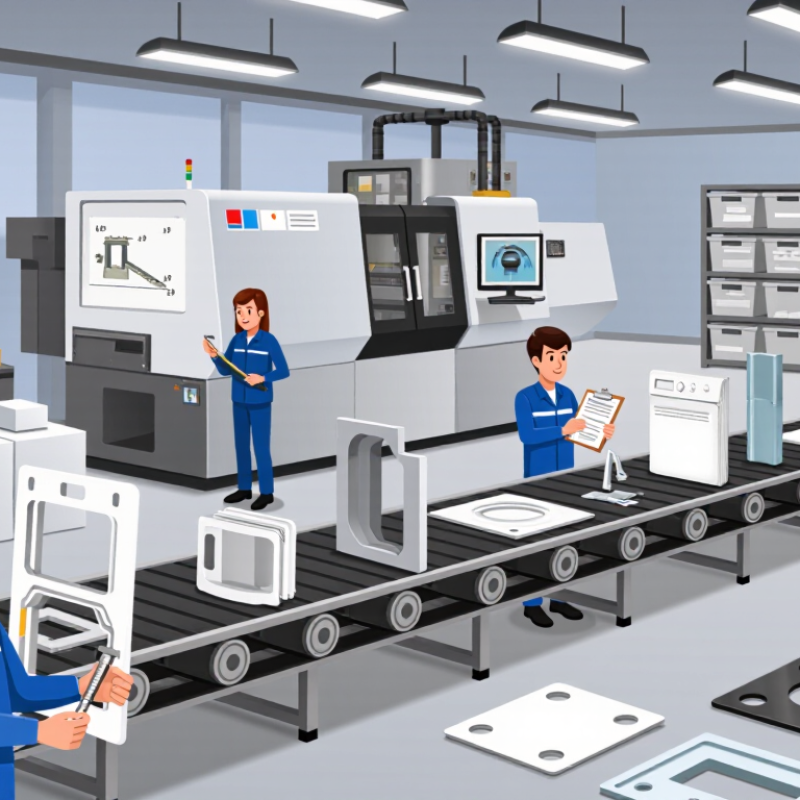
In 2022, global plastics production reached about 400.3 million tonnes, according to industry estimates. That scale matters when evaluating appliance injection parts. These are molded plastic components made by injecting heated material into a shaped tool, then cooling it to form a repeatable part. Examples include control-panel bezels, refrigerator drawer rails, washing-machine buttons, and small clips that hold wiring in place.
The process can produce detailed shapes with consistent dimensions across large production runs. A supplier can adjust resin selection, wall thickness, and tool design to meet practical needs such as impact resistance or heat exposure. A door handle, for instance, faces different stresses from an internal cable guide. The details matter.
For global sourcing, injection-molded parts may offer predictable production and efficient shipping when designs are standardized. Buyers should still check sample fit, material data, surface finish, and quality-control records. Ask how changes to a tool or resin will be documented. Small issues can become costly after parts reach an assembly line. Plastic production totals alone do not show whether a component is durable or responsibly made. That remains a gap worth examining, especially when comparing suppliers across regions.
Compare Resin and Molding Processes Using ISO 20400 Sustainable Procurement Principles
For global appliance sourcing, compare resin and molding routes against ISO 20400’s guidance on lifecycle impacts, supplier transparency, and responsible purchasing. ISO 20400 is guidance, not a product certification. Ask suppliers for resin origin, recycled-content evidence, process-energy data, and scrap rates. Small details matter: a pellet grade can change part weight, cycle time, and reject volume.
The scale is significant. PlasticsEurope’s Plastics—The Fast Facts 2023 reports:
400.3 million tonnes of global plastics production in 2022; circular plastics represented 8.9 percent.
These figures make material choices hard to dismiss. Recycled resin may reduce demand for virgin feedstock, but performance and traceability must be verified for each appliance component.
Compare injection-molding suppliers using energy per kilogram of acceptable parts, not machine capacity alone. Check mold design, cooling time, regrind controls, and transport distance. A lighter component can help. Yet poor yield may erase the gain.
We should admit that supplier data is sometimes incomplete; request consistent measurements and review them over time.
Qualify Suppliers Through ISO 9001:2015 Quality Systems and Process-Capability Data
When sourcing appliance injection-molded parts globally, an ISO 9001:2015 certificate is a useful starting point, not a guarantee of consistent parts. Ask how the supplier applies its quality system to your specific components. Review inspection records, material traceability, mold maintenance logs, and procedures for handling nonconforming parts. Details matter. A clear record should connect a resin batch to a production date and inspection result.
Process-capability data can show whether critical dimensions remain stable across production runs. For a molded housing, this might include measurements of snap-fit width, wall thickness, or mounting-hole position. Request the sampling method, measurement equipment, and recent results—not only a single capability score. Confirm that the study reflects the intended mold, material, machine, and production conditions. Otherwise, polished figures may describe a process you will never receive.
During supplier qualification, compare capability data with your drawing tolerances and assembly needs. Ask what happens when a trend moves toward a limit, even if parts still pass inspection. In practice, a supplier may have strong paperwork but incomplete data for a new mold. That is worth discussing openly. Pilot runs, agreed control plans, and periodic reviews can reveal gaps before regular shipments begin. No system removes all variation; the goal is to understand it and respond consistently.
Verify Market Access Against RoHS’s 10 Restricted Substance Categories and REACH
Why Choose Appliance Injection Parts for Global Sourcing?
For appliance injection parts, market access depends on more than a resin specification. RoHS restricts ten substance categories, including lead, cadmium, mercury, and certain phthalates. Pigments, stabilizers, and recycled content can affect a molded part’s composition. A small color change may also mean a different formulation. Check the rules that apply to each destination; requirements and exemptions can vary.
Tips: Request a current material declaration for each part number. Match reports to the exact resin, color, and production site. Keep test records and supplier change notices together. REACH has a broader scope: review relevant restrictions and the Candidate List of substances of very high concern, which can change over time. A passing RoHS report does not automatically establish REACH compliance.
In practice, verify documentation before approving samples for a new market. Ask how suppliers control incoming materials and notify buyers about formulation changes. Independent testing can help resolve gaps, especially for parts with several additives or multiple sources. Paperwork can look complete and still miss a detail. That is worth checking twice.
Why Choose Appliance Injection Parts for Global Sourcing?
Verify market access against RoHS’s 10 restricted substance categories and REACH requirements.
RoHS limits shown are maximum concentrations by weight in homogeneous materials: 0.1% for nine categories and 0.01% for cadmium. Applicable exemptions may affect specific uses. REACH has separate obligations, including restrictions and duties related to substances on the Candidate List; this chart does not assess REACH compliance.
Sources: EU RoHS Directive 2011/65/EU, Annex II, as amended; European Chemicals Agency (ECHA), REACH Candidate List.
Compare Landed Cost, Lead Time, and Supply Risk Across Global Sourcing Regions
For appliance injection parts, the quoted unit price is only one piece of the sourcing decision. Landed cost also includes tooling, packaging, freight, duties, inspection, and the cost of carrying inventory. A lower factory price can lose its appeal when parts travel farther or arrive in large, inflexible batches. Compare quotes using the same resin grade, tolerances, annual volume, and delivery terms. Small differences matter. A heavier carton can raise freight costs across thousands of shipments.
Lead time depends on more than distance. Tool changes, material availability, production capacity, and port congestion all affect delivery. A nearby supplier may offer faster replenishment, while a distant region may provide attractive pricing but require longer planning windows. Ask for a realistic production schedule, not just a standard lead-time figure. For critical parts, confirm whether capacity is reserved and how schedule changes are communicated. The answer may be less tidy than the quotation.
Supply risk deserves the same attention as cost. Check whether the mold, resin supply, and key production steps depend on a single location. Regional diversification can reduce exposure to transport delays, but it may add qualification work and quality variation. Request sample inspection records and define measurable acceptance criteria before scaling orders. No sourcing region is risk-free. Even a carefully reviewed plan can miss a disruption, so keep a practical buffer for parts that could stop assembly.
Why Choose Appliance Injection Parts for Global Sourcing?
Compare indicative landed-cost, lead-time, and supply-risk considerations across sourcing regions for appliance injection-molded parts.
Basis and limitations: Figures are indicative planning ranges, not supplier quotations or audited market averages. The landed-cost index uses China as a relative reference point of 100 and assumes comparable part specifications, order volumes, tooling requirements, quality standards, and delivery to a major customer market. Lead times are broad production-and-transport planning estimates and vary by route, season, capacity, and shipping method. Actual comparisons should include duties, freight, packaging, inspection, inventory carrying cost, and supplier-specific quality performance.