How to Choose the Best Wire Harness Machine?
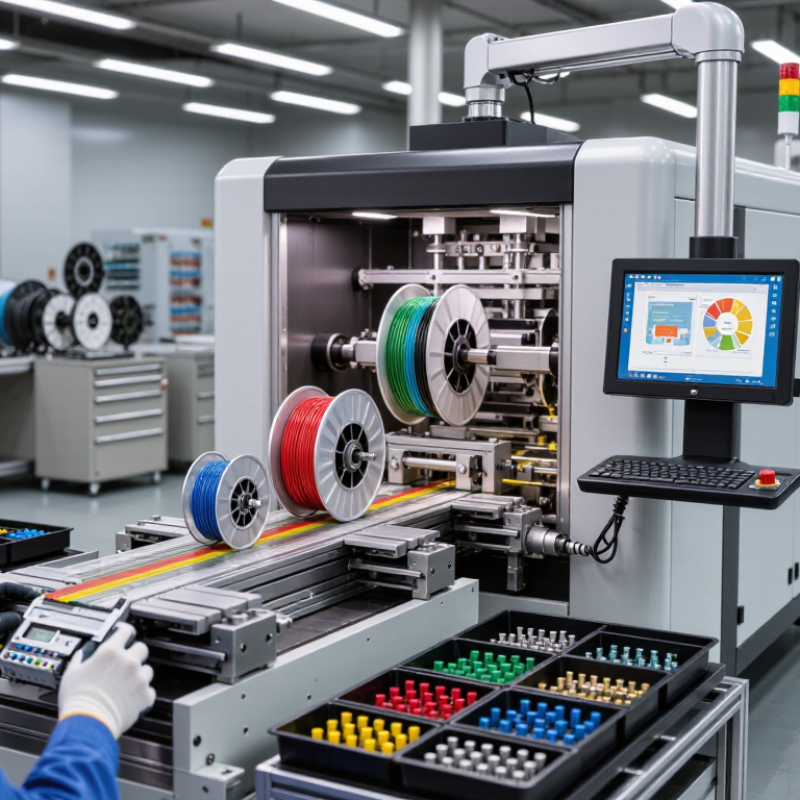
Choosing the best wire harness machine starts with a clear picture of the work it must perform. A machine suited to short custom runs may not meet the needs of a high-volume production line. Identify the wire types, gauges, insulation materials, and connector styles you use every day. Then check whether the equipment can cut, strip, crimp, mark, or process wires in the sequence your workflow requires.
For example, a production team handling several wire sizes may value quick changeovers as much as fast cycle times. A stable crimp matters. Poorly matched tooling can cause inconsistent connections, even on a capable machine. Small details matter. Ask suppliers about adjustment ranges, safety features, maintenance access, spare parts, and operator training. Request a sample run using your own wire and terminals when possible. Test before buying. Measure the results, inspect the crimps, and note how much setup the run takes.
There is no universally best wire harness machine; the right choice depends on product mix, output targets, floor space, and operator experience. Automation can reduce repetitive work, but it does not remove the need for process checks or skilled setup. Compare total ownership costs, not just the purchase price. Clear documentation and responsive technical support can make a real difference when a line stops. Some specifications look impressive on paper, yet prove less useful in daily production. That is worth questioning. A careful evaluation helps buyers choose equipment that fits current jobs while leaving room for realistic growth.
Match the Machine’s AWG and mm² Range to Your Wire Specifications
How to Choose the Best Wire Harness Machine?
Match the Machine’s AWG and mm² Range to Your Wire Specifications
A machine’s listed wire range should match the conductors you actually process, not just the sizes on a future project plan. AWG uses smaller numbers for thicker wire, while mm² describes conductor cross-sectional area. For reference, 18 AWG is about 0.82 mm², and 16 AWG is about 1.31 mm². These figures help with comparison, but they do not tell the whole story.
Check the machine’s minimum and maximum capacity against every wire size in your production mix. Then verify whether the range applies to solid or stranded conductors, and whether insulation diameter or wire construction affects feeding and stripping. Two wires with the same AWG can behave differently in the guides and blades. It is easy to overlook that detail when comparing specification sheets. Request a trial with your actual wire, including the smallest and thickest sizes, and inspect cut length, strip quality, and conductor damage before choosing.
Tips: Keep a written AWG-to-mm² reference beside your sample list. Confirm the exact wire types with the supplier, and allow room for production variation. A listed range is a starting point, not proof of a clean result.
How to Choose the Best Wire Harness Machine?
Match the machine’s AWG and mm² range to your wire specifications.
The chart shows approximate conductor cross-sectional areas for common AWG sizes. Before selecting a machine, confirm that its supported wire range covers your smallest and largest wires. Also check insulation diameter and the machine’s feeding, cutting, and stripping capabilities, since AWG and mm² describe the conductor—not the insulated wire’s overall diameter.
Compare Rated Output in Wires per Hour and Setup Time
How to Choose the Best Wire Harness Machine?
Compare rated output in wires per hour with the setup time needed to achieve it. A machine rated at 1,200 wires per hour may look fast, but that figure can reflect a steady run with one wire type and few interruptions. Peak rate misleads. Ask how the rate changes when operators switch wire gauges, cut lengths, strip settings, or terminal applicators.
Time setup from the last conforming wire of one job to the first conforming wire of the next. Include material loading, recipe selection, adjustments, and quality checks. Small batches expose it.
Use actual run data, not a brochure number. For a planning check, applying a 60% operating-efficiency assumption to a 1,200-wire-per-hour rating gives about 720 wires per hour. Vorne’s OEE Industry Benchmark identifies roughly 60% as typical and 85% as world-class manufacturing OEE; these are broad references, not wire-harness guarantees.
Compare machines using the same test: identical wire, terminals, batch size, and acceptance criteria. Record several changeovers, since one unusually smooth setup proves little. Ask for both average setup time and the slowest observed run. The result may be less tidy than a single rating, but it is more useful for staffing and delivery estimates.
Assess Crimp Quality Against IPC/WHMA-A-620 Requirements
How to Choose the Best Wire Harness Machine?
Assess Crimp Quality Against IPC/WHMA-A-620 Requirements
A wire harness machine should produce crimps that meet documented acceptance criteria, not merely look tidy. IPC/WHMA-A-620E (2022) defines three product classes, with acceptance expectations suited to different end uses. Choose equipment that can hold stable crimp height and force settings, and retain setup records.
Small defects matter. A single loose strand or poorly supported insulation can undermine an otherwise clean connection.
During trials, inspect conductor brush, bellmouth, insulation support, and strand damage under consistent lighting. Measure crimp height with a calibrated tool, then compare results with the terminal manufacturer’s specification and the applicable IPC class. There is no universal crimp-height target; terminal geometry matters. One approved sample is not enough. Run repeated cycles and check variation across operators, wire sizes, and shifts.
Ask for evidence, not promises: sample measurements, changeover records, and results from pull testing where required by the control plan. IPC/WHMA-A-620 provides acceptance criteria, but it does not replace process validation for a specific terminal and wire combination. A machine may pass a short demonstration yet drift during production. That possibility is easy to overlook. Keep inspection findings and machine settings together, so quality teams can trace a failed crimp back to its setup.
Verify Continuity, Short-Circuit, and 100% Electrical-Test Capabilities
A wire harness machine should prove every circuit, not merely move wires through a fixture. Check that its tester detects open circuits, shorts between pins, and miswires. Ask how it handles resistance limits and connector pin maps. A clear display helps, but stored test results matter more. Small details matter. Confirm that each finished harness receives an electrical test, rather than relying on batch sampling. The test voltage and limits must match the harness specification; excessive voltage can damage sensitive components.
Deloitte and MAPI’s 2019 Smart Factory study found that 86% of manufacturing executives expected smart factory solutions to drive competitiveness within five years. The study was not specific to harness testing, but it highlights why test data and automation deserve attention. Look for a machine that records pass/fail results against each harness identifier and flags failures by circuit. A practical check: test a known-good harness, then introduce a controlled open or short and confirm the system catches it. Do not assume a polished report proves sound test coverage. Review the fixture contacts, operator prompts, and retest rules; worn contacts can create intermittent failures that are easy to miss.
Compare Tooling Costs, Uptime, and Cost per Finished Harness
Choosing a wire harness machine by purchase price alone can hide its real cost. Compare tooling, setup labor, maintenance, scrap, and usable output over the same production period. Include applicators, blades, dies, changeover kits, and calibration. A machine with inexpensive tooling may require frequent adjustments. That difference matters when short runs fill the schedule.
Uptime needs a practical definition: scheduled production time minus unplanned stops. Track stoppages by cause, not just total hours. The U.S. Department of Energy’s Operations & Maintenance Best Practices guide reports predictive maintenance can reduce maintenance costs by 8–12% compared with preventive maintenance, and downtime by 35–45%. These are broad industry estimates, not a guarantee for harness production. Ask suppliers for documented cycle and changeover data, then test with your wire sizes and terminal types. Small details count.
Calculate cost per finished harness as total operating cost divided by accepted harnesses, not machine cycles. Include labor, tooling wear, energy, scrap, and rework. For example, a fast cycle is less valuable if crimp-height checks create a queue. I would also leave room for uncertainty: estimates often miss operator learning time. A spreadsheet can look precise while the shop floor disagrees. Compare a representative production run, and record good units, stops, and setup minutes before deciding.
| How to Choose the Best Wire Harness Machine? — Compare Tooling Costs, Uptime, and Cost per Finished Harness |
| Production setup |
Typical initial tooling cost (USD) |
Assumed machine cost (USD) |
Availability (uptime) |
Rated output (harnesses/hour) |
Effective output (harnesses/hour) |
Estimated cost per finished harness (USD) |
Best fit |
| Manual cut, strip, and hand-crimp bench |
$500 |
$2,000 |
90% |
25 |
22.5 |
$3.51 |
Low-volume work, frequent product changes, and simple harnesses |
| Semi-automatic cut, strip, and crimp cell |
$4,000 |
$18,000 |
92% |
70 |
64.4 |
$2.84 |
Steady production where flexibility and reduced labor are both important |
| Automatic cut, strip, and crimp machine |
$12,000 |
$65,000 |
85% |
180 |
153 |
$3.05 |
High-volume, repeatable wire processing with sufficient demand to use the capacity |
Planning assumptions: Illustrative USD estimates for a simple four-wire harness with eight crimps. Effective output equals rated output multiplied by uptime. Cost per harness includes $2.40 of wire and terminal materials, direct labor at $24 per hour, tooling amortization, machine depreciation, and estimated maintenance. Tooling is amortized over 100,000 harnesses for the manual and semi-automatic setups and 250,000 for the automatic setup; machine depreciation assumes 10,000 operating hours. The model assumes accepted output and excludes scrap, rework, tax, financing, and downstream harness assembly. Actual costs and performance vary with product design, tooling, labor rates, utilization, and supplier quotations.